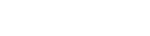The global transition toward renewable energy has placed a significant spotlight on the industrial capabilities of East Asia, particularly regarding the scale and efficiency of photovoltaic production. As nations strive to meet net-zero emissions targets, the role of specialized manufacturers has become pivotal in reducing the cost of solar energy while increasing the energy density of installations. Understanding the landscape of high-efficiency module production is essential for developers looking to maximize their return on investment.
Technological breakthroughs in cell architecture, such as the shift from standard PERC to TOPCon technology, have redefined what is possible in terms of energy conversion. This evolution allows for higher power output from a smaller physical footprint, making solar energy viable for constrained urban environments and massive utility-scale farms alike. The ability to mass-produce these high-spec components ensures that sustainable energy is no longer a luxury but a scalable global standard.
When sourcing high-performance hardware, partnering with experienced solar system manufacturers in china ensures access to cutting-edge Monocrystalline technology and robust supply chains. By leveraging advanced manufacturing processes, these partners provide the reliability and efficiency required to sustain long-term energy projects across diverse climatic zones.

Technical Innovation of TOPCon Solar Modules
The introduction of TOPCon (Tunnel Oxide Passivated Contact) technology has revolutionized the energy harvest capabilities of modern panels. By utilizing a thin tunnel oxide layer, these modules significantly reduce recombination losses at the contacts, allowing the SBM-10-144-585W to achieve a conversion efficiency of 21.65%. This technical leap ensures that more photons are converted into usable electricity, even in suboptimal lighting conditions.
For project developers, this increased efficiency translates directly into lower balance-of-system (BOS) costs. Because each panel generates more power, fewer modules are required to reach the target capacity, reducing the amount of racking, cabling, and land usage. This makes the integration of high-spec modules from leading solar system manufacturers in china a strategic advantage for maximizing land-use efficiency.
Core Components of High-Efficiency Solar Systems
A high-performance solar system relies on the synergy between high-purity silicon crystals and robust structural materials. Monocrystalline cells are the gold standard here, as their single-crystal structure allows electrons to flow more freely than in polycrystalline alternatives. This fundamental material advantage is what enables peak power ratings of 585W in the SBM-10-144 series, providing a dense energy source for various applications.
Beyond the cells, the mechanical integrity of the module is paramount for long-term operation. The use of high-transmit, low-iron tempered glass ensures maximum light penetration while providing a shield against environmental stressors. Combined with an anodized aluminum-alloy frame, these components allow the panels to withstand mechanical loads up to 5400pa, making them resilient against heavy snowfall and extreme wind pressures.
Electrical stability is further managed through a maximum system voltage of 1500V DC and high-quality series fuse ratings of 25A. These specifications ensure that the modules can be safely integrated into large-scale arrays without risking electrical failure or degradation. The meticulous engineering of these components allows for a stable power output across a wide temperature range, from -40℃ to +85℃.
Global Applications for Industrial Solar Modules
The versatility of the SBM-10-144-585W makes it suitable for a vast array of global deployment scenarios. In residential settings, the sleek dark aesthetic and high efficiency allow homeowners to maximize limited roof space while maintaining architectural beauty. In commercial sectors, warehouse rooftops are transformed into power plants, helping businesses meet green building standards and reduce operational overhead.
Large-scale utility solar farms benefit most from the scalability offered by solar system manufacturers in china. By deploying bifacial dual-glass options, these farms can capture reflected light from the ground (albedo), significantly increasing the total energy yield per square meter. This is particularly effective in sandy or snowy regions where ground reflectivity is high.
Furthermore, these modules are increasingly used in remote industrial zones and off-grid installations. When paired with Battery Energy Storage Systems (BESS), they provide a reliable, autonomous power source for mining sites, telecommunication towers, and disaster-relief centers. The ability to maintain performance in low-light conditions ensures that critical infrastructure remains powered regardless of the weather.
Performance Comparison: Mono vs Poly Systems
When comparing Monocrystalline TOPCon modules to traditional Polycrystalline panels, the difference in energy yield is stark. Monocrystalline cells, used by top-tier solar system manufacturers in china, typically offer conversion efficiencies exceeding 21%, whereas Polycrystalline panels often linger between 15% and 17%. This gap represents a significant loss of potential energy over the lifespan of a project.
Beyond efficiency, the degradation rate is a critical factor for long-term investment. Monocrystalline modules are engineered for longevity, often retaining over 80% of their original capacity after 25 years. In contrast, older poly-technology often sees faster degradation, leading to a slower recovery of the initial investment and higher replacement costs over time.
Energy Efficiency Rating: Mono TOPCon vs Standard Poly
Long-Term Stability and Durability Standards
The operational lifespan of a solar installation is dictated by its ability to withstand environmental degradation. The SBM-10-144-585W is specifically engineered to combat the effects of PID (Potential Induced Degradation) and LID (Light Induced Degradation), ensuring that the power output remains stable over two and a half decades. This stability is a hallmark of the quality control processes implemented by leading solar system manufacturers in china.
Mechanical durability is further reinforced by the use of high-grade aluminum alloys that prevent corrosion in humid or saline environments. Whether installed in a coastal region or a high-altitude mountain range, the combination of tempered glass and a robust frame ensures the cells are protected from micro-cracks and moisture ingress, maintaining the 1500V DC system integrity under the most challenging conditions.
ROI Maximization in Utility-Scale Solar Projects
For PV developers, the Return on Investment (ROI) is calculated by the ratio of energy production to the total cost of installation and maintenance. By utilizing modules with 21.65% efficiency, the land requirement is minimized, which directly lowers the cost of land acquisition and site preparation. High energy density means that a smaller array can produce the same megawattage as a larger, less efficient system.
Operational efficiency is also boosted by the low-maintenance design of these modules. The high-transmit glass resists dirt accumulation and withstands cleaning cycles, reducing the frequency of manual upkeep. When these factors are combined with the long-term power guarantee, the payback period for the installation is significantly shortened compared to standard polycrystalline setups.
Integration with smart monitoring and tracking systems further accelerates ROI. By optimizing the angle of the SBM-10-144-585W throughout the day, operators can squeeze every possible watt from the sunlight. This synergy between hardware excellence and digital optimization ensures that the project remains profitable and sustainable throughout its 25-year lifespan.
Future Trends in Photovoltaic Manufacturing
The future of the industry is moving toward "Ultra-Efficiency," where N-type TOPCon and HJT (Heterojunction) technologies will become the baseline. We are seeing a shift toward bifacial-as-standard, allowing for energy capture from both sides of the panel. This trend is driven by solar system manufacturers in china who are constantly pushing the boundaries of silicon purity and cell geometry.
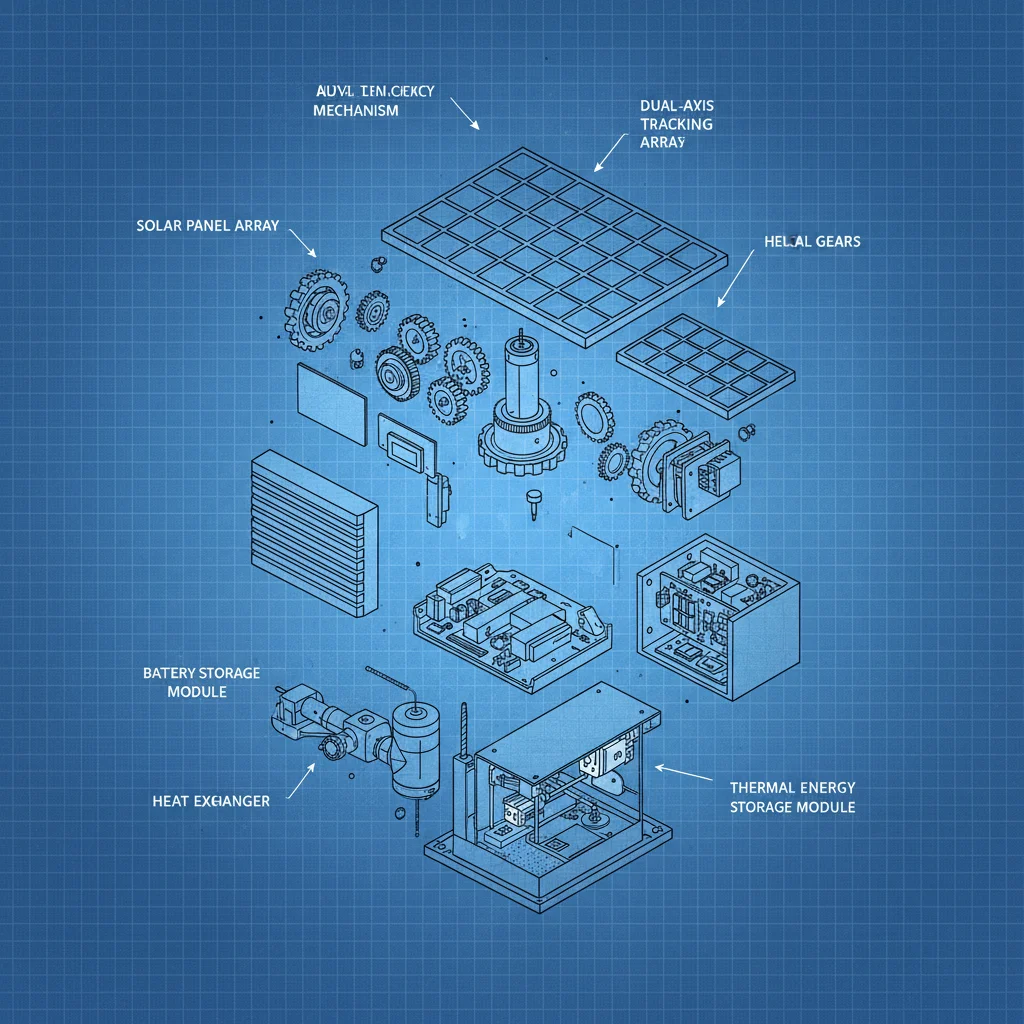
Digital transformation is also playing a role, with AI-driven production lines reducing waste and increasing the precision of cell slicing. This automation ensures that every module leaving the factory meets strict tolerance levels (0~+5W), eliminating the risk of underperforming panels within a large string, which can otherwise bottleneck the entire system's output.
Sustainability in manufacturing is the final frontier. The industry is shifting toward "Green Factories" that use recycled aluminum and carbon-neutral energy to produce the panels themselves. This creates a truly circular economy where the means of production are as sustainable as the energy the final product generates.
Comparison of Solar Technology Evolutions and Impact
| Technology Era |
Average Efficiency |
Primary Benefit |
ROI Speed |
| Standard Poly |
15% - 17% |
Low Initial Cost |
Slow |
| Standard Mono PERC |
18% - 20% |
Better Space Use |
Moderate |
| N-Type TOPCon |
21% - 23% |
Ultra-High Yield |
Fast |
| Bifacial Dual-Glass |
22% - 25% (Total) |
Rear-side Capture |
Very Fast |
| HJT Technology |
23% - 26% |
Low Temp Coeff. |
Fast |
| Tandem Perovskite |
28% - 30%+ |
Theoretical Limit |
Emerging |
FAQS
Monocrystalline panels, such as the SBM-10-144, are crafted from a single, pure silicon crystal. This structure allows electrons to move more freely, resulting in higher energy conversion rates (typically 20-24%) compared to the fragmented crystal structure of polycrystalline cells. This leads to a higher wattage per square inch, which is critical for projects with limited installation space.
Yes. Monocrystalline silicon cells, especially those utilizing TOPCon technology, maintain more stable performance in low-light conditions and cloudy weather. They can capture a broader spectrum of light, ensuring a more consistent power output during early mornings, late evenings, or overcast days compared to other panel types.
Monofacial panels capture sunlight only on the front side. Bifacial dual-glass panels are designed to capture sunlight from the front and reflected light from the rear. This can significantly increase total energy yield, especially when installed on reflective surfaces like white roofs or light-colored gravel, making them a favorite for utility-scale farms.
High-quality mono panels are engineered for exceptional longevity. Most are designed to operate for 25 years or more. Due to the stability of the TOPCon cells and the durability of the aluminum frames, they typically retain over 80% of their original power capacity even after a quarter-century of exposure to the elements.
Absolutely. Their high efficiency makes them ideal for off-grid systems where space is limited and maximizing the energy harvest is critical for powering homes and charging battery banks. Their ability to perform in diverse lighting conditions ensures a more reliable power supply for remote installations.
The SBM-10-144-585W is built to handle a maximum mechanical load of 5400pa. This high rating means the panel is highly resistant to extreme wind pressure and heavy snow accumulation, preventing structural failure or cell micro-cracking in harsh climates.
Conclusion
The transition to a sustainable energy future depends heavily on the ability to deploy high-efficiency, durable, and cost-effective photovoltaic solutions. By combining TOPCon cell technology with robust mechanical construction, the SBM-10-144-585W provides a scalable answer to the world's growing energy demands. From maximizing ROI for utility developers to providing reliable off-grid power for homes, the synergy of high conversion rates and long-term stability is the key to successful solar adoption.
As we look toward the next decade, the role of leading solar system manufacturers in china will continue to be central to driving down the cost of energy while pushing the limits of efficiency. For those looking to optimize their energy portfolio, investing in N-type monocrystalline technology is no longer just an option—it is a strategic necessity for long-term sustainability and profitability. Visit our website to learn more: www.shaobosolar.com